Food Business Solutions

Maheu Production Process: How to Improve Production at Scale

Scaling up maheu production involves more than increasing vessel size. As batch volumes rise, powder addition, cooking, cooling and fermentation must work together to deliver a consistent beverage at the required throughput.
Book a Consultation

Maheu, also known as mahewu, is a fermented cereal beverage commonly made from maize.  Recipes and fermentation methods vary across regions and manufacturers, but successful industrial production starts with a repeatable cooked base.

Understanding where the maheu production process becomes constrained helps manufacturers improve capacity without compromising texture, flavour or process control.

The main stages of maheu production

Traditional preparation generally involves dispersing maize meal in water, cooking it into a porridge, cooling to between 27-35◦C, for traditional methods and adding a fermentation source. Fermentation develops the characteristic acidity and flavour. Commercial methods need to translate these stages into a defined, validated process. Some manufacturers are now by passing this process and simply adding and fermented/acidic flavouring to save the long fermentation process. 

  • Maize preparation and dosing

Maize meal is checked against the required raw material specification and measured with the recipe water. Particle size and composition can influence hydration and heating times.

  • Dispersion and cooking

The meal is incorporated into water and heated under controlled mixing parameters. Cooking and agitation develops the cereal base.

  • Cooling and fermentation preparation

The cooked base is cooled to the temperature required by the selected fermentation method.

  • Fermentation

Traditional methods may use cereal flour or malt as a source of fermentation microorganisms; commercial processes may use selected starter cultures. Temperature, time and acidification need to be controlled against the manufacturer’s validated specification.

  • Finishing and filling

Depending on the product, subsequent stages may include sweetening, flavour addition, stabilisation, cooling or further heat treatment. These stages depend on the intended shelf life, storage conditions and whether live cultures are to remain in the finished beverage.

There is no single cooking or fermentation schedule suitable for every maheu recipe.

Why a small-batch method may struggle at industrial scale

A process that works in a small vessel may become difficult to reproduce at several thousand litres.

Powder may accumulate faster than the mixing system can disperse it. As maize cooks and the base thickens, circulation and heat transfer can become more demanding. A larger vessel with insufficient product movement can develop uneven processing conditions, while prolonged heating against hot surfaces can contribute to fouling or burn-on which contaminates the entire batch. 

Manual additions also become a capacity constraint. If operators load many bags individually, ingredient addition may occupy a substantial part of the cycle and vary between batches.

Manufacturers should examine the complete sequence: loading, dispersion, heating, any required hold, cooling, transfer and cleaning. Increasing heating capacity alone will have limited value if the vessel still waits for powder loading or an available fermentation tank.

Control the cooked base before fermentation

The cooked base establishes the starting conditions for the next stage. Variation in solids content, cooking history or dispersion can produce differences in viscosity and texture before fermentation begins.

Useful controls include the maize-to-water ratio, powder addition rate, mixing conditions, temperature profile and any required holding stage. These should be developed for the actual meal grade, recipe finished product quality and equipment.

Mixing needs to distribute incoming powder and maintain product movement as viscosity changes. Simply increasing agitator speed does not necessarily resolve poor circulation or inadequate powder wetting.

Consistency should be assessed using defined measurements. These may include solids content, viscosity and sensory checks, with samples compared at a consistent temperature and under the same test conditions.

Faster powder addition must deliver effective dispersion

A dedicated powder induction system can reduce reliance on adding bags directly into a cooking vessel. It introduces powder into a moving liquid stream, helping combine ingredient addition and dispersion.

The important measure is the time required to produce an acceptably dispersed base. Loading powder quickly offers little benefit if extended mixing is then needed to remove agglomerates.

Powder addition rate must therefore be matched to liquid flow, solids concentration and the system’s ability to handle the developing viscosity. Controlled weighing and a defined addition sequence help maintain the intended formulation.

Where in-line processing and Jet Cook can help

An in-line cooking arrangement processes product as it passes through the heating system,  within a recirculating batch configuration. This can concentrate heating and mixing duties in a controlled flow path.

A Jet Cook system can support rapid heating, powder entrainment, shear and mixing of the maize base, with powder induction and recipe control incorporated where appropriate. The configuration needs to reflect the required solids content, viscosity, thermal treatment and production rate.

Putting scale-up into practice: Take 5

At Take 5 in South Africa, four Multi In-Line Jet Cook™ units combine fast simultaneous heating, shearing and controlled recirculation to rapidly cook and hydrate the maize base. Thermal energy transfers directly into the product, supporting controlled heating and consistent maize gelatinisation.

A 1,000-litre powder induction system incorporates 600 kg of maize flour in two minutes, shortening the ingredient addition stage. Recipe Manager controls the production sequence, including ingredient additions, temperatures, shear and processing times, helping operators reproduce the approved method.

The installation produces 6,000 litres in 20 minutes, using a single processing vessel operated by one person within a 4 × 7 metre footprint.

The practical lesson is that capacity comes from coordinating powder incorporation, cooking and process control. Improving these stages together can increase output while limiting manual intervention and making efficient use of factory space. These installation figures relate to preparation of the cooked base; cooling and fermentation capacity must still be matched to this output.

Read the full Take 5 case study.

Match cooking capacity to cooling and fermentation

Faster cooking increases output only when the rest of the process can accept the product.

Cooling capacity must be sufficient to prepare the base for fermentation at the required rate. Fermentation vessel capacity must account for the fermentation duration, filling and emptying sequence, cleaning and production schedule.

Fermentation should be assessed against defined acceptance criteria, including the relevant pH or acidity measurements, rather than elapsed time alone. Hygienic transfer, suitable cultures and controlled operating conditions remain essential; rapid cooking does not replace fermentation control.

For manufacturers assessing an expansion, trials should establish base quality and process requirements before final capacity is specified. DC Norris combines Jet Cook technology, powder handling and product and process expertise to help develop larger, more repeatable maheu production systems.
V1-JDRGroup-DC Norris - CTAs -650x363px-DD-18Dec2024-01


The post Maheu Production Process: How to Improve Production at Scale appeared first on DC Norris.
Read More

Manufacturing Recipe Management Software for Reducing Food Waste

In batch food production, waste can begin with a small deviation: an ingredient outside its weighing tolerance, an addition made at the wrong temperature or a holding stage extended beyond the approved process.

Book a Consultation

The result may be a product outside its required viscosity, solids content, flavour or texture specification. Even where recovery is possible, rework consumes ingredients, operator time and energy, while occupying equipment needed for the next batch. Further ingredient additions or processing adjustments may also take the product outside its approved formulation or quality assurance limits.

Manufacturing recipe management software can help reduce these losses by translating an approved formulation and processing method into a controlled sequence. Its value depends on the quality of the recipe, the accuracy of the instrumentation and how effectively deviations are managed.

The manufacturing process turns a recipe into a finished product

A recipe specifies the ingredients and their proportions. The manufacturing process defines how those ingredients are combined and treated to achieve the required finished product.

This includes the order of addition, mixing conditions, heating stages, target temperatures and holding times. Controlling these parameters alongside ingredient quantities is essential for repeatable product quality.

This distinction matters. A timed heating stage and a temperature-based transition are not interchangeable. Where a validated process requires a hold at a specified temperature, the control logic needs to define when that hold begins and how a temperature deviation is handled.

Food recipe control software should therefore reflect the actual process requirements, with clear operator prompts and automatic controls where suitable equipment is connected.

Ingredient tolerances should reflect product sensitivity

Applying the same percentage tolerance to every ingredient may be inappropriate. A deviation in bulk water and an equivalent percentage deviation in a functional ingredient can have very different consequences.

Tolerances should account for the ingredient’s effect on product specification, the quantity being added and the capability of the weighing or metering system. Small additions may require separate weighing arrangements if the vessel load cells cannot reliably resolve them.

Where integrated verification is available, the control system can check an addition against its permitted range before allowing the sequence to continue. However, weight verification alone does not establish ingredient identity; preparation controls and ingredient identification remain essential.

Automatic scaling reduces manual calculation when batch size changes, but scaling ingredient quantities does not establish suitable processing conditions for the new batch. Mixing performance, heat-up time and working volume need to be assessed separately.

Sequence control protects product quality

Repeatability requires control of the order and conditions of processing, as well as ingredient quantities and addition stages. This is particularly relevant where ingredients hydrate, thicken or respond differently to heat and mixing.

Practical example: starch dispersion in a sauce

Consider a sauce process that specifies preparing a starch slurry and adding it at a defined stage under controlled mixing.

If dry starch is added directly instead, or the specified dispersion stage is missed, the batch may develop lumps and uneven thickening. The outcome depends on the starch type, formulation and processing conditions; starches should not all be treated as having the same addition requirements or temperatures.

Attempting to recover the batch through extended mixing or additional heating may consume more energy and damage the product, without restoring the required texture. Further ingredient adjustments can also alter the formulation and final yield.

A controlled process can specify the preparation method, prompt the addition at the correct stage and apply the approved mixing and heating sequence. It helps prevent a known process error rather than relying on correction once the defect has developed.

This is an illustrative production scenario, not a reported customer case study.

Manufacturing recipe management software in a food production facility, with operators monitoring automated processing equipment through a digital control panel.

Stuart Rigby, Product and Process Manager at DC Norris, explains why process control is essential to reducing recurring batch problems: 

“When investigating an inconsistent batch, we need to look at how the ingredients were processed, as well as what was added. Addition order, dispersion, temperature and mixing conditions can all affect the result. Recipe control helps operators repeat the approved method and gives the process team a record of deviations, so recurring problems can be investigated rather than repeatedly corrected.”

Record actual conditions, not only recipe settings

A stored process describes what should happen. A batch record needs to show what actually happened.

Useful records include ingredient weights, measured temperatures, stage durations, operator actions and deviations, linked to the relevant batch and recipe revision. Recording actual conditions allows production and quality teams to compare an acceptable batch with one requiring investigation.

For example, a viscosity difference may prompt a review of ingredient additions, heat-up duration and mixing stages. The records can narrow the investigation, although they do not establish the cause on their own.

Recorded production data supports food safety checks when reviewed against validated limits and the site’s HACCP procedures. Complete traceability also requires links to ingredient lots and subsequent product handling. A completed recipe sequence alone is not sufficient evidence for batch release.

Use batch data to target avoidable losses

The resource benefit of better control comes from reducing preventable deviations and unnecessary processing.

Additional heating or mixing uses energy and equipment capacity. Rework requires labour and may introduce further ingredients. Rejected product also carries the resource cost of its original manufacture and replacement production.

Manufacturers can assess improvement by monitoring:

  • First-time batch acceptance and rework rates.
  • Ingredient deviations and their recurring causes.
  • Actual yield against expected yield.
  • Processing time and energy use per kilogram of acceptable product.

Comparisons should account for product type and batch size. A shorter cycle is not an improvement if it compromises the required treatment or product quality.

Keep process under controlled review

Effective food production software needs approved process stages, controlled revisions and defined permissions for changes. Temporary adjustments should be recorded and reviewed, rather than becoming undocumented practice.

Recipe limits should also be achievable with the installed equipment and verified instruments. Software can help enforce a sound manufacturing method, but it cannot compensate for an unsuitable process or unreliable measurement.

DC Norris combines Recipe Manager software with product, process and equipment expertise to help manufacturers establish controlled production sequences and investigate batch performance.

V1-JDRGroup-DC Norris - CTAs -650x363px-DD-18Dec2024-01


The post Manufacturing Recipe Management Software for Reducing Food Waste appeared first on DC Norris.

Read More

5 Common Mistakes When Using Industrial Cooking Systems

Modern industrial cooking systems give food manufacturers greater control over temperature,agitation, processing times, product quality and recipe consistency.

BOOK A CONSULTATION


But even the most advanced equipment will only perform as well as the process behind it.

Through product trials, commissioning, operator training and ongoing process support, the DC Norris team sees first-hand how relatively small processing decisions can affect batch times, product quality and overall efficiency.

Here are five common mistakes and how manufacturers can avoid them.

1. Using the Wrong Heating Method

Not every product should be heated in the same way.

Traditional steam-jacketed vessels remain highly effective for many applications, but relying solely on jacket heating isn’t necessarily the most efficient approach for every product or process.

For applications where rapid heating and effective mixing are important, technologies such as Jet Cook™ can provide an alternative approach, rapidly transferring heat into the product while simultaneously heating, mixing, and pumping.

The important consideration is the product itself, required temperature, batch size, viscosity, particulate integrity and target processing time. The heating method should be selected around the process rather than simply because it is how the product has always been cooked.

The lesson: Match the heating technology to the process, rather than making the process fit the equipment.

2. Using the Wrong Agitator Settings

Agitation is about much more than keeping ingredients moving.

Agitator type and speed can influence heat transfer, ingredient incorporation, product texture and consistency. Running too slowly may result in inadequate mixing or uneven heating, while excessive agitation can negatively affect products containing delicate particulates.

Settings may also need to change during different stages of the same recipe. The optimum agitation during initial heating, for example, may not be appropriate once particulates or other sensitive ingredients have been added.

Understanding what is happening to the product at each stage allows operators to select settings based on the process rather than relying on one speed throughout.

3. Adding Ingredients at the Wrong Time

Ingredient sequence can have a significant influence on the finished product.

Adding an ingredient too early, too late or missing a stage altogether can change how ingredients hydrate, disperse or react with one another. Temperature at the point of addition can be equally important.

In a busy production environment, experienced operators can sometimes develop their own way of doing things. Small deviations may initially appear insignificant but can introduce variation between operators, shifts and batches.

Clearly defined recipes and automated process stages can help ensure ingredients are added at the correct point every time.

4. Not Understanding How Ingredients Behave

Knowing the recipe isn’t necessarily the same as understanding the process.

Starch is a good example. Different starches respond differently to temperature, water, percentages, shear and processing time. Introducing starch at an inappropriate stage, applying the wrong level of agitation or using an unsuitable heating profile can affect hydration, viscosity and final product texture.

Similar considerations apply to gums, proteins, fats, powders and other functional ingredients.

This is one reason product trials can be so valuable. Testing ingredients under realistic processing conditions allows manufacturers to establish the optimum sequence, temperature, mixing and heating method before moving into full production.

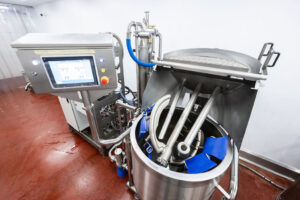
Industrial cooking systems used for preparing food in a commercial production environment.

DC Norris Customer Trials Example

During a customer trial in South Africa, the DC Norris team identified that inconsistencies in the customer’s finished product were not being caused by the equipment itself, but by the sequence in which ingredients were being added and processed.

The customer was producing sweet chilli sauce and experiencing significant variation in finished product viscosity from batch to batch. A review of the manufacturing process revealed that sugar was being added before the starch had fully hydrated. Because sugar absorbs available water very quickly, it was limiting the amount of free water available for starch activation, resulting in inconsistent thickening and a less predictable finished product.

Working with the customer, the team redesigned the process sequence. Water and starch were added first and heated to approximately 72°C to achieve around 90% starch activation before the sugar was introduced. This allowed the starch sufficient time to hydrate and develop the desired viscosity before competing ingredients were added.

The revised process delivered a far more consistent sauce and demonstrated how small adjustments to ingredient addition, heating profiles and agitation can significantly improve product quality.

Importantly, the new process was then built into the system’s recipe controls, ensuring the sequence could be repeated automatically in production rather than relying on individual operator judgement. The result was a robust, repeatable process capable of delivering an in-specification product batch after batch.

Key takeaway: Consistency isn’t achieved by running the same recipe every time. It’s achieved by having the flexibility and process control to adapt the recipe when product behaviour demands it.

5. Bypassing Automated Recipe Controls

Automation is designed to make a successful process repeatable.

Yet there can be a temptation for experienced operators to override automated stages, manually adjust settings or bypass recipe controls because they know the product.

The problem comes when different operators make different adjustments.

A Recipe Manager can control key parameters such as processing times, ingredient addition time, temperatures, agitation settings and processing stages, helping manufacturers reproduce an established process consistently across batches and shifts.

Automation doesn’t replace operator knowledge. Instead, it captures a successful process and helps make it repeatable.

DC Norris has seen this principle in practice. In one published trial, two operators following the same traditional curry recipe produced visibly different results because decisions such as onion softening and the amount of agitation were based on individual judgement. By moving to a defined Jet Cook™ and Recipe Management process, the cooking stages, temperatures and holding times could be controlled and recorded, creating a more repeatable process.

Industrial cooking systems with automated controls in a commercial food manufacturing facility.

Getting the Process Right

Many problems attributed to industrial cooking equipment aren’t necessarily equipment problems at all.

They can result from the interaction between the equipment, ingredients, recipe and operator.

That’s why DC Norris takes a process-led approach to industrial cooking systems. Customers can carry out trials in our Product Development Kitchens, test recipes using their own ingredients and work with our team to establish the most appropriate processing method.

That support continues through commissioning and hands-on operator training at the customer’s site — and can continue throughout the life of the system as recipes, operators and production requirements change.

“Getting the best from an industrial cooking systems isn’t just about reaching the right temperature. You need to understand how the product behaves throughout the process — when ingredients are added, how they’re mixed and how the heating method affects them. That’s often where relatively small changes can make a significant difference.”

[Stuart Rigby – Product & Process Manager]

The objective isn’t simply to automate a recipe.

It’s to understand the process well enough to make it efficient, consistent and repeatable.

V1-JDRGroup-DC Norris - CTAs -650x363px-DD-18Dec2024-01

The post 5 Common Mistakes When Using Industrial Cooking Systems appeared first on DC Norris.

Read More